Quality Control
Foil Balloon Quality Control Checklist Before Shipment
Foil balloon quality control should verify the approved product and pack—not merely count cartons. A useful inspection plan defines defect classes, sampling, test methods, references and shipment-release authority before production begins.
Counting pieces is the easiest part of inspection. The expensive failures are often elsewhere: the wrong color under the right label, barcodes linked to the wrong SKU, valves that are difficult to use, print shifts, missing accessories, weak seals or retail cards packed with the wrong balloon. Those problems can survive a superficial final check.
FoilJoy treats pre-shipment QC as a confirmation of the approved commercial product, not a carton-counting exercise. Product, function, print, packaging, barcode and carton data all need to agree before release. The buyer should receive what was approved—not merely the right number of boxes.
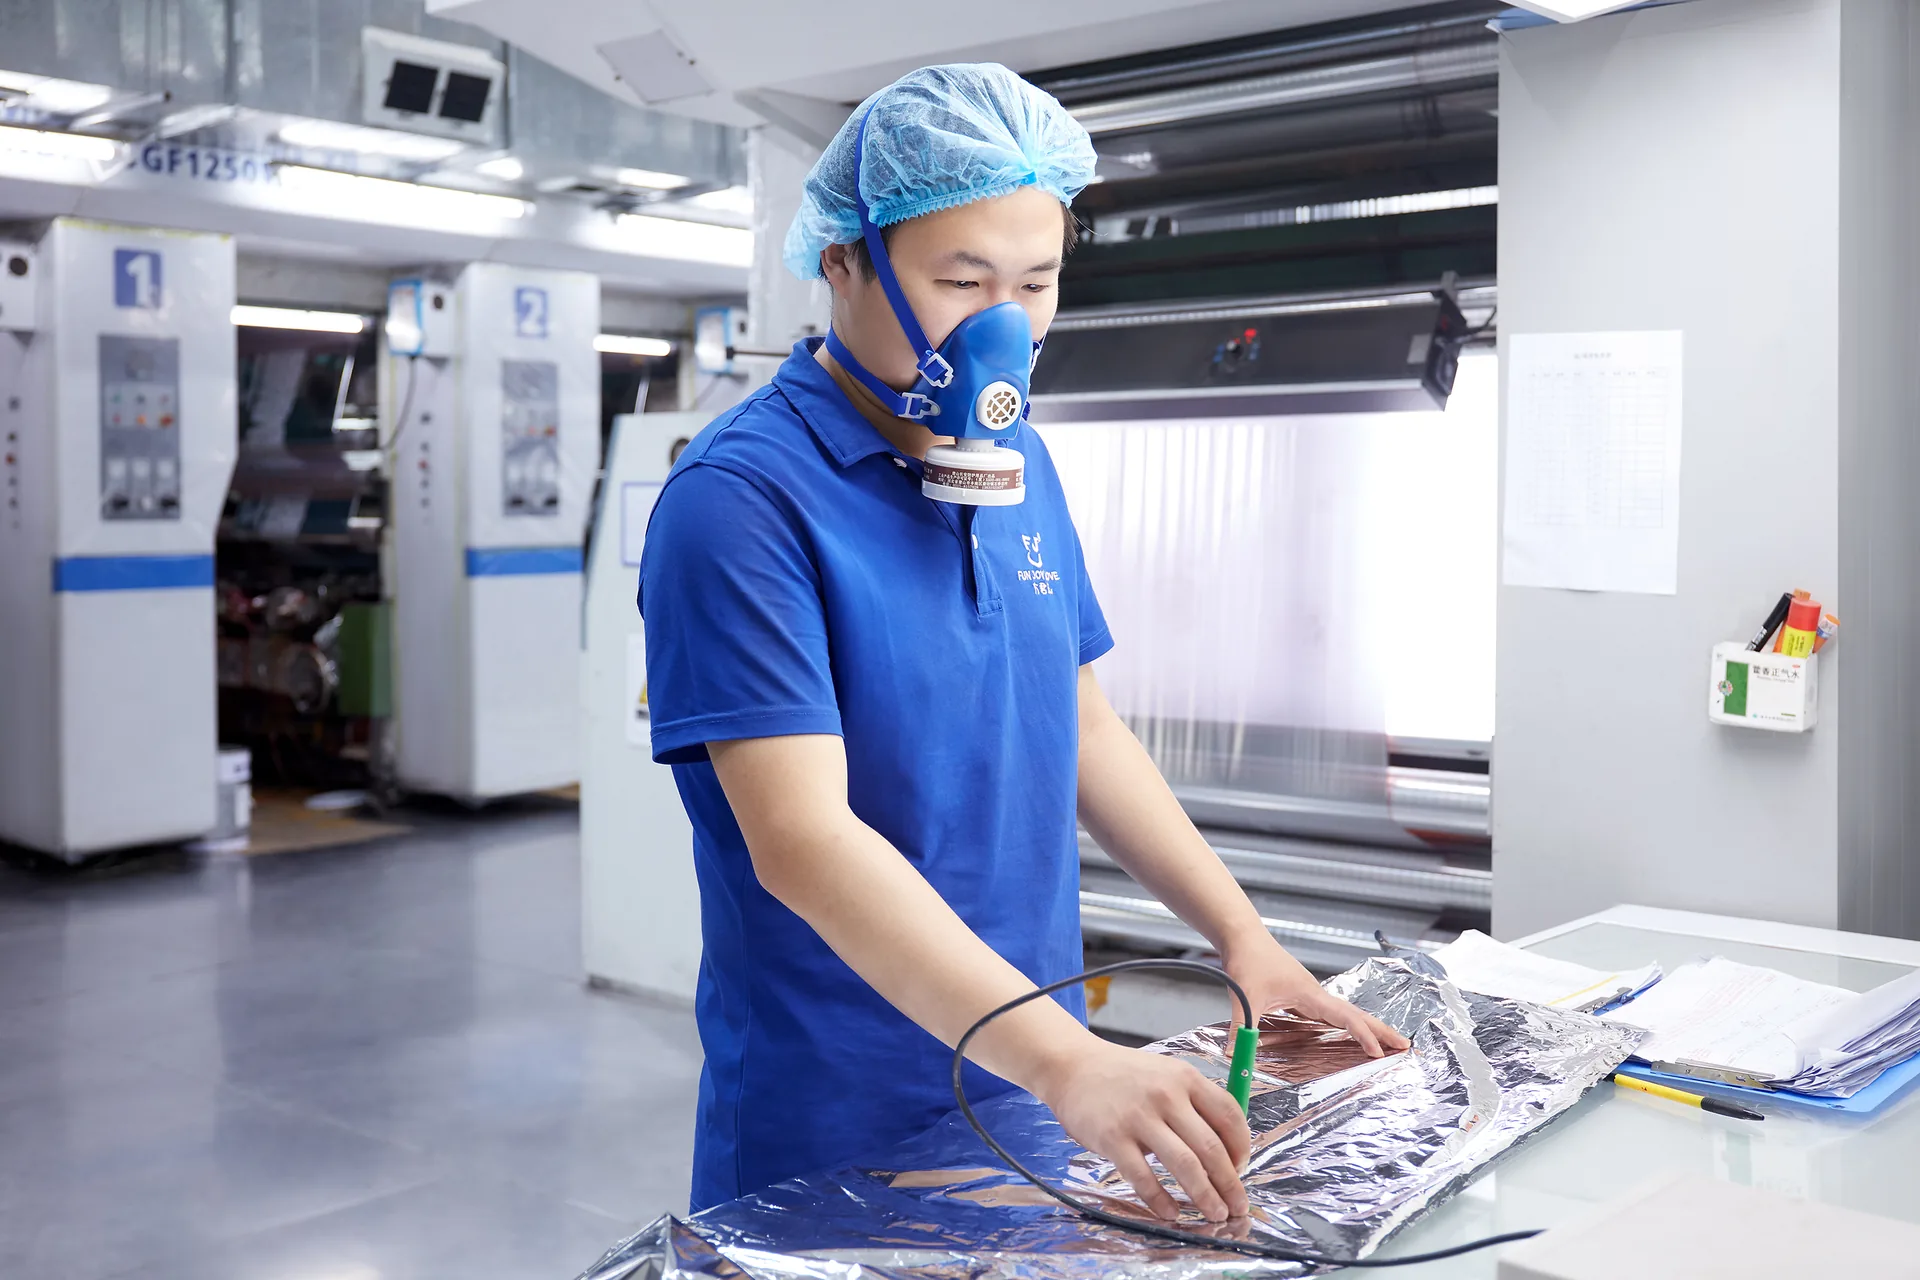
1. Freeze the reference set
The inspector needs the signed specification, approved artwork version, golden sample or dated sample photos, packaging files, assortment ratio, carton marks and purchase order. If two references disagree, production should not guess. Name one document hierarchy and one decision owner.
2. Define defects by customer impact
| Class | Examples to define for your SKU |
|---|---|
| Critical | Safety or regulatory issue, wrong market warning, prohibited contamination or severe misuse risk |
| Major | Leak, failed valve, wrong artwork, unusable pack, missing accessory, barcode failure |
| Minor | Small cosmetic variation outside the approved visual tolerance but not affecting use |
Classifications must be agreed for the actual product. For statistical inspection concepts, use the official ISO overview of the ISO 2859 acceptance-sampling system and obtain the relevant standard or professional advice for your plan.
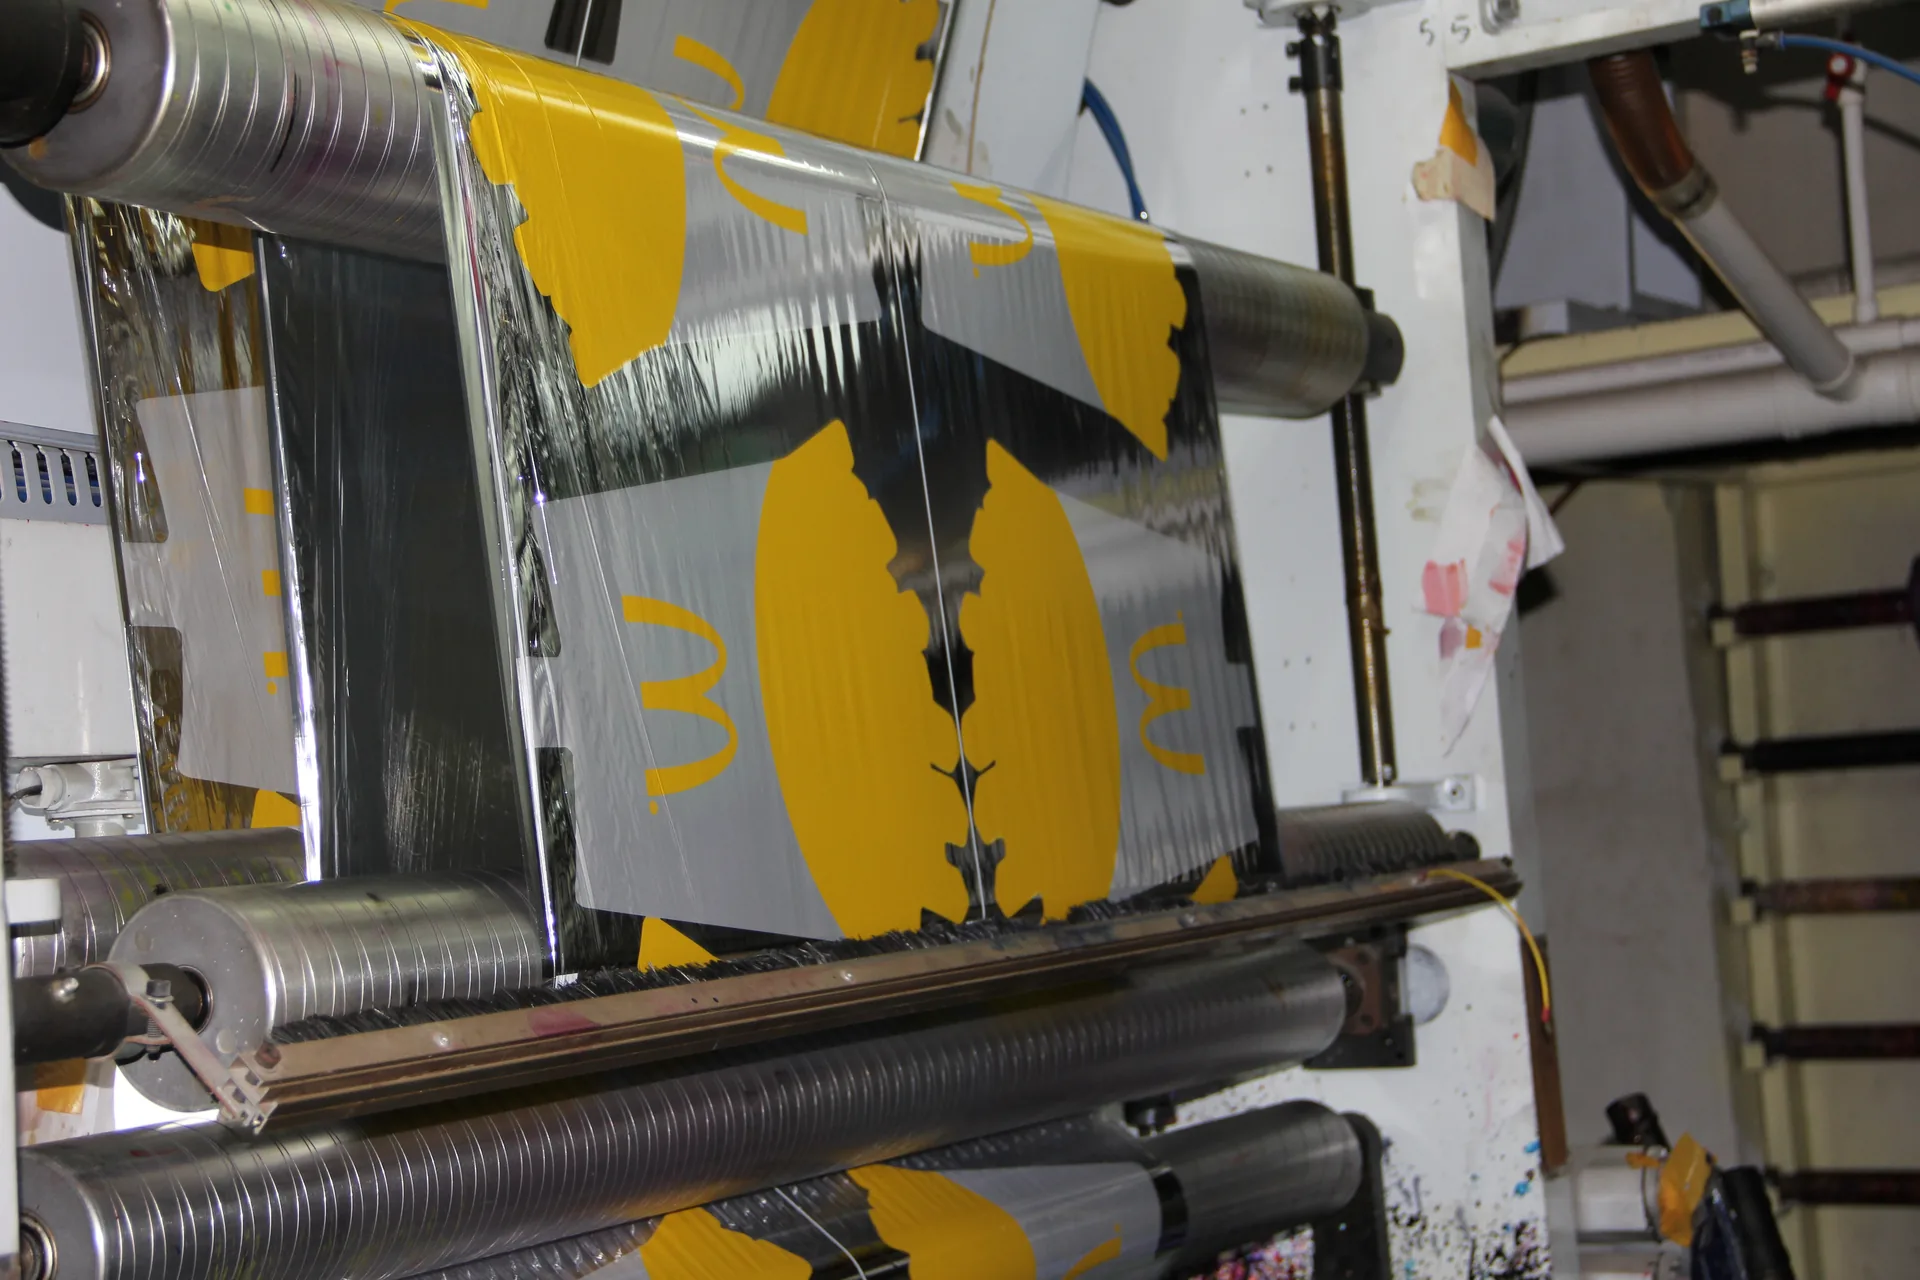
3. Inspect product attributes
Visual and dimensions
Shape, size, print registration, color, scratches, wrinkles, contamination, cut edge and orientation.
Seals and valve
Perimeter continuity, internal seam position, seal burn, weak spots, valve alignment and insertion access.
Inflation performance
Sample inflation, chamber communication, appearance, valve closure, leak checks and agreed retention evaluation.
Accessories
Correct straw, stick, cup, ribbon, weight or handle; attachment and safety reviewed as specified.
4. Inspect retail packaging
- Correct SKU and artwork version.
- Accurate quantity and assortment.
- Legible instructions, warnings and responsible-party information.
- Barcode printed and scanned against the item record.
- Clean seals, aligned cards and sound peg holes.
- No accessory placement that can puncture the balloon.
5. Inspect master cartons and shipment data
Verify carton quantity, gross and net weight tolerance, dimensions, shipping marks, lot identification, carton condition and total count. Compare physical results with the packing list. Photograph random open cartons and the container loading pattern when required.
6. Use a release workflow
- Inspector issues a report with sample IDs and photos.
- Supplier segregates nonconforming goods.
- Buyer reviews defects against agreed classifications.
- Corrective work is documented and rechecked.
- Authorized person issues written shipment release.
US retailer responsibilities do not end at the factory gate
The CPSC provides a practical overview of retailer product-safety responsibilities. The importer and retailer should maintain traceability, manage complaints and act on safety information after sale.
Get a factory review before you commit
Send FoilJoy your artwork, target market, quantity, packaging and deadline. We will review production feasibility and prepare a clear next step for a foil balloon inspection and quality plan.
Continue your buying research
Browse every guide in the FoilJoy News & Buyer Insights hub, or see our OEM factory capabilities.
FAQ
Is final inspection enough?
No. Upstream material, print, seal and first-article controls reduce the chance of discovering systemic defects after packing.
What is AQL?
It is part of an acceptance-sampling approach. The buyer must define the plan, lot, sample and defect thresholds correctly.
Should every balloon be inflated?
Usually inspection uses an agreed sample plus production process controls. The correct plan depends on risk and specification.
Who releases shipment?
Name an authorized buyer representative in the purchase order or quality agreement.